Selecting the right filtration medium often involves a critical trade-off between structural integrity and permeability. In high-precision industrial environments, the demand for materials that can withstand specific chemical exposures while maintaining consistent flow rates has led to a deeper reliance on specialized polymers.
The shift toward engineered porosity allows for tighter control over particle retention and fluid dynamics, moving beyond simple mesh screens toward integrated material solutions. This technical evolution is particularly evident in sectors requiring sterile environments or high-temperature resilience, where traditional materials often fail.
Understanding the mechanical properties and selection logic of porous plastic products is essential for engineers aiming to optimize system efficiency and reduce long-term maintenance costs.


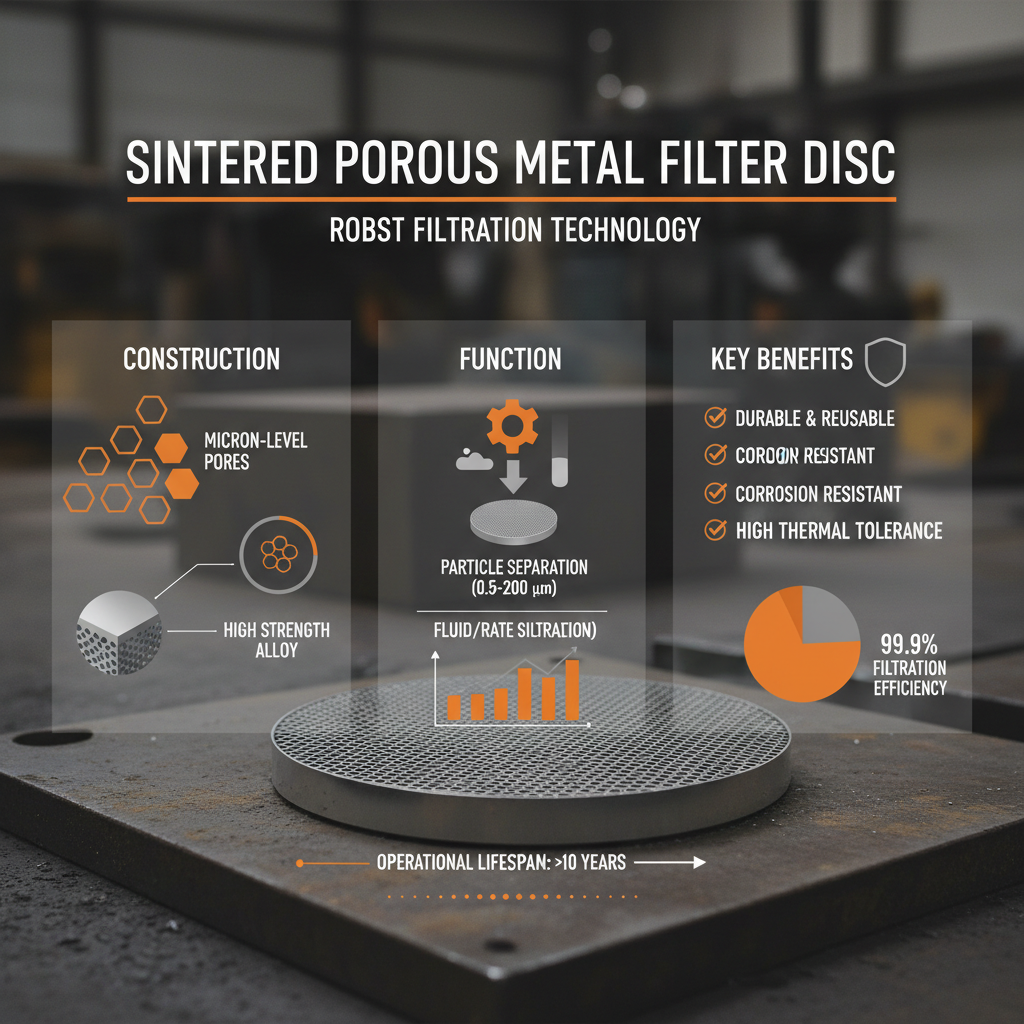
Unlike traditional molded plastics, sintered porous materials are created by fusing polymer particles under controlled heat and pressure. This process ensures that the material does not melt completely, leaving behind a network of interconnected voids that allow fluids to pass through while capturing contaminants.
The choice of polymer—ranging from PE and PP to more advanced fluoropolymers—determines the chemical compatibility and thermal limits of the final component. This versatility makes these materials indispensable in environments where metallic filters would corrode or where organic membranes lack the necessary mechanical strength.
The efficacy of a filter is governed by its pore size distribution. In the production of sintered plastics, engineers control the initial powder grain size and the sintering temperature to dictate the final porosity. A narrow distribution ensures consistent filtration efficiency, whereas a wider distribution may be preferred for depth filtration applications where high dirt-holding capacity is required.
Mechanical strength is the second pillar of design. While increasing porosity generally improves flow rates, it can compromise the structural integrity of the part. Achieving the "sweet spot" requires a precise balance of thermal bonding and void space, ensuring the filter can withstand operational pressure spikes without collapsing or shedding particles into the filtrate.
Advanced manufacturing techniques now allow for graded porosity, where the pore size changes across the thickness of the material. This design minimizes the pressure drop by allowing larger particles to be captured in the outer layers while the finer internal layers handle the final polish of the fluid.
Evaluating a porous filter requires looking beyond the nominal micron rating. Engineers must consider the "bubble point," which defines the largest pore through which air can be pushed, and the permeability coefficient, which quantifies the ease with which a fluid passes through the medium.
Operational success depends on the synergy between high porosity for throughput and precise pore architecture for retention; one cannot be optimized at the total expense of the other without compromising system longevity.
Furthermore, the chemical resistance of the polymer matrix is a non-negotiable factor. Whether dealing with aggressive solvents or medical-grade disinfectants, the material must maintain its geometric stability and pore openness over thousands of cleaning cycles.
The relationship between porosity and flow resistance is typically non-linear. As the percentage of void space increases, the flow rate rises significantly, but the ability to capture microscopic particles decreases. For most industrial applications, a porosity range of 60% to 90% is targeted to balance these opposing needs.
In practical terms, a filter with 88% porosity will exhibit a much lower pressure drop than one with 80%, making it ideal for high-volume throughput where absolute particle removal is less critical than flow efficiency.
In a typical industrial setting, such as a medical laboratory or a chemical processing plant, these filters serve as the primary defense against cross-contamination. For example, in laboratory filtration, the requirement for zero leaching and high chemical purity makes sintered plastic the preferred choice over metal alternatives.
Conversely, in automotive or heavy machinery applications, the focus shifts toward particulate removal in diesel or gasoline filters. Here, the ability to handle high flow rates while maintaining a specific porosity—often around 80% to 88%—is critical for protecting downstream components from wear and tear.
The industry is moving away from generic filtration membranes toward application-specific engineered materials. We are seeing a rise in the use of composite sintered structures that combine the strength of metal fibers with the chemical resistance of polymers, creating hybrid filters that perform across wider temperature and pressure ranges.
Digital twins and computational fluid dynamics (CFD) are now being used to model the internal flow of porous plastics before they are manufactured. This allows for the optimization of pore geometry to eliminate "dead zones" within the filter, thereby increasing the effective filtration area and extending the service life of the component.
Sustainability is also driving innovation, with a push toward recyclable high-performance polymers. The goal is to maintain the strict technical parameters required for medical and industrial use while reducing the environmental footprint of the manufacturing process.
Choosing the correct porous medium requires a systematic evaluation of the operating environment. Buyers should first define the maximum allowable pressure drop and the minimum particle size that must be retained. Only then can the specific porosity and material type be determined.
It is a common error to prioritize "high porosity" without considering the structural load. In high-pressure systems, a slightly lower porosity (e.g., 80% vs 88%) can provide the necessary mechanical stability to prevent deformation, which would otherwise lead to filtration bypass.
As a professional integrated enterprise, POROYAL utilizes its expertise in powder sintered technology to provide tailored solutions. By analyzing the specific requirements of the application—whether it is for medical lab filters or heavy-duty particulate filters—the right balance of material and porosity can be engineered.
| Application Priority | Recommended Porosity | Material Focus | Primary Constraint |
|---|---|---|---|
| Max Flow Rate | 85% - 90% | High-Grade Polymer | Mechanical Strength |
| Fine Retention | 60% - 75% | Dense Sintered Plastic | Pressure Drop |
| Chemical Resistance | Variable | Fluoropolymers (PTFE) | Material Cost |
| High Temp Stability | 70% - 85% | Specialized Sintered Alloy | Thermal Expansion |
| Medical Sterility | 80% - 88% | Medical Grade PP/PE | Leachables/Extractables |
| General Industrial | 80% - 85% | Standard Sintered Plastic | Service Life |
Sintering involves heating polymer powder to a temperature where particles bond at their contact points without fully melting. This preserves the gaps between particles, creating an interconnected network of pores. Traditional molding creates a solid, non-porous mass. Sintering is the only way to achieve a structural, permeable plastic body with precise, controllable void spaces for filtration purposes.
Increasing porosity typically reduces the flow resistance (pressure drop) and increases the throughput of the system. However, it usually results in a larger average pore size, which may reduce the filtration efficiency for very fine particles. Additionally, higher porosity can lead to a slight decrease in the overall compressive strength of the filter element.
Yes, many sintered plastic products are designed for reuse. Depending on the material, they can be cleaned via back-flushing, ultrasonic cleaning, or chemical washing. The durability of the sintered bond ensures that the pore structure remains intact during these processes, provided the cleaning agents are chemically compatible with the specific polymer used.
Plastic sintered filters are preferred when the application involves corrosive chemicals that would attack stainless steel, or when weight reduction is critical. They are also essential in medical and laboratory settings where metallic ions must be completely excluded from the process to prevent contamination of sensitive samples.
The most reliable method is the Bubble Point Test, which measures the pressure required to force air through the liquid-filled pores. Other methods include scanning electron microscopy (SEM) for visual verification of pore geometry and permeability testing using a standardized fluid to calculate the flow rate per unit area.
Temperature limits vary wildly by polymer. Standard PE or PP may only withstand up to 80-120°C. However, specialized sintered materials can handle much higher temperatures. For extreme heat, such as burner mediums or exhaust systems, metal sintered options are used, with some capable of resisting temperatures up to 900°C.
The engineering of porous plastic products is a precise science that balances the physics of fluid flow with the chemistry of polymers. By moving away from generic solutions and focusing on specific porosity and material compatibility, industrial operators can significantly improve the reliability and efficiency of their filtration systems.
Whether deploying in a medical lab or an automotive particulate system, the key to success lies in a rigorous selection process that accounts for pressure, temperature, and chemical exposure. Investing in precision-engineered sintered solutions ensures long-term operational stability and optimal performance.