Premium Pipette Filters Factory Leading China Suppliers of Sintered Lab Filters
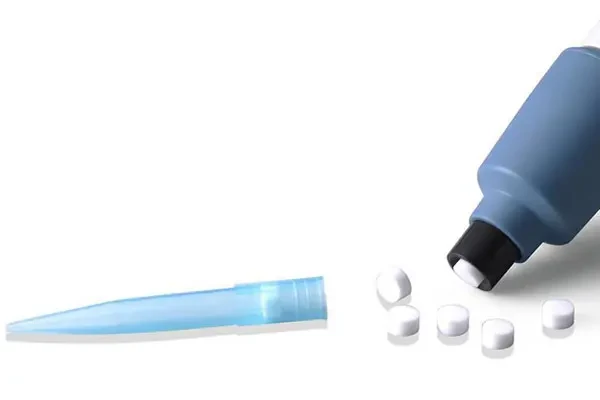
Our premium Pipette Filters are engineered for high-precision laboratory environments, providing an essential barrier against aerosol contamination. Designed specifically for medical and research applications, these filters ensure that your samples remain pure and your laboratory personnel are protected from hazardous biological agents, adhering to the strictest standards of environmental pollution prevention.
Utilizing advanced porous materials, our filtration technology optimizes the balance between airflow resistance and retention efficiency. Whether used in molecular biology or clinical diagnostics, these filters prevent liquid carry-over and cross-contamination, ensuring the integrity of every microliter handled during critical analytical processes.
Detailed Parameters
| Material Type | High-Grade Polypropylene / Sintered Porous Material | Filter Diameter | Customizable per Pipette Brand |
|---|---|---|---|
| Filtration Rating | Hydrophobic / Aerophilic Grade | Compatibility | Universal Lab Pipette Systems |
| Temperature Limit | -20°C to +121°C (Autoclavable) | Chemical Resistance | Acid, Base, and Organic Solvent Resistant |
| Sterilization | Gamma Irradiated or EO Sterilized | Flow Rate | Low-Resistance High-Throughput |
| Certification | ISO 9001 / CE Compliant | Application | Medical, Lab, and Bio-Pharm |
Key Advantages
Anti-Contamination
Effective aerosol barrier that prevents sample carry-over and protects against laboratory cross-contamination.
High Durability
Engineered with sintered porous materials for extended life and structural integrity under pressure.
Precision Fit
Strict dimensional tolerances ensure a perfect seal with pipette tips, eliminating air leakage.
Low Air Resistance
Optimized pore structure allows smooth liquid aspiration without hindering pipetting speed.
Chemical Inertness
Non-reactive materials ensure no leaching of contaminants into sensitive medical samples.
Standard Compliance
Manufactured according to strict medical and lab filter industry standards for global exports.
Product Gallery


Management Platforms
Quality Inventory Control
Real-time tracking of filter batches to ensure 100% traceability of medical-grade materials.
Precision Molding Tech
Advanced CNC and sintering processes for consistent pore size distribution across all units.
Compliance Monitoring
Continuous auditing based on environmental protection and laboratory safety regulations.
Sterilization Protocol
Rigid sterile packaging management to prevent any external contamination during transit.
Custom Order System
Flexible manufacturing platform to accommodate specific pore sizes and material requests.
After-Sales Support
Dedicated technical support for integrating filters into diverse automated lab systems.
Investment Return Comparison
| Feature Metric | Standard Filters | Our Sintered Pipette Filters |
|---|---|---|
| Sample Purity Rate | Moderate | Ultra-High (99.9%+) |
| Operational Lifespan | Short / Single-use | High Durability / Extended Use |
| Contamination Risk | Medium | Negligible / Zero Leakage |
| Maintenance Cost | Frequent Replacement | Reduced Long-term Expenditure |
| Laboratory Safety | Basic Protection | Maximum Biological Barrier |
Frequently Asked Questions
We use high-grade polypropylene and specialized sintered porous materials that are inert to most organic solvents, acids, and bases used in environmental and medical labs.
Our filters create a hydrophobic barrier that allows air to pass through while blocking liquid droplets and aerosols from entering the pipette shaft.
Yes, we offer customizable dimensions to ensure a precision fit for all industry-standard pipettes, ensuring no air leakage during operation.
Absolutely. Our materials are heat-resistant up to 121°C, making them fully compatible with standard autoclave sterilization cycles.
Sintered porous filters offer more uniform pore distribution, higher mechanical strength, and superior filtration efficiency compared to basic molded plastics.
Yes, our manufacturing process follows ISO 9001 standards, and our products are designed to meet strict environmental and safety guidelines for lab equipment.
Ready to Enhance Your Lab's Filtration Precision?
Contact Us